When tiny traces change the story
The problem starts at the margin: a faint residue on a collet, an unnoticed coolant break, a micro-abrasion on a chuck face. Over months those margins conspire into failure rates and mysterious rejects. The tools and protocols that worked for short runs reveal gaps in long-term endurance, and solutions displayed at the international medical expo often point to both kit and process shifts rather than a single gadget. In a problem-driven frame, the job is to find the hidden vectors before they become a pattern.
Why contamination hides in precision work
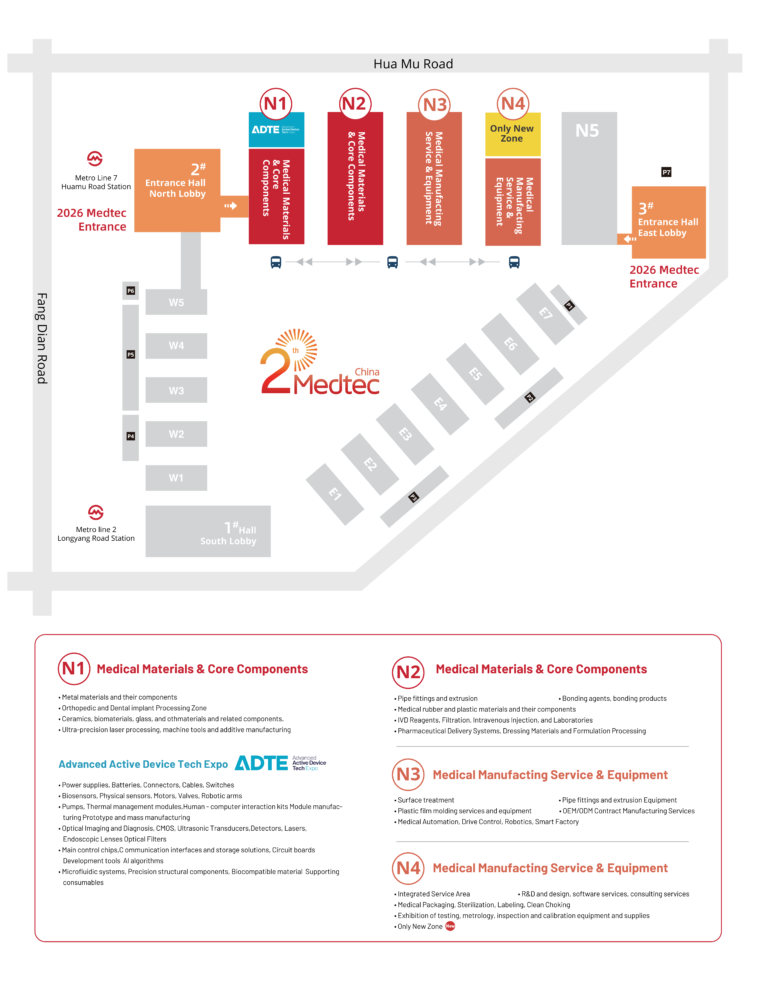
Swiss machining trades on repeatability, micron tolerances and tight tolerances. That reliability breeds complacency — surfaces get reused, setups drift. At a Medtec live demonstration I noted vendors showing filtration upgrades and torque-controlled spindles; the detail mattered more than the headline. Real-world anchors like ISO 13485 requirements remind teams to document control points and keep traceability. Contamination lives in tool changeovers, coolant cycles and human touch. Catching it requires sensing where the process changes imperceptibly.
Hard controls that actually reduce failure rates
Start with containment and measurement. Implement procedure gates where parts change hands, and log those transfers. Use dedicated fixtures for high-risk families and a token system to prevent cross-use. Calibrate torque on chucks and toolholders weekly. Clean coolant with staged filtration and scheduled media replacement. Add in-process checks that measure form or surface finish rapidly rather than relying only on end-of-run inspection. Track trends with simple SPC charts tied to machine hours and tool life.
Tests, retention and real checks
Actionable verification must include both physical and biological checks where applicable. For medical-contact components, retain a sample lot with bioburden testing — note the 14-day incubation limit for standard bioburden assessment. Maintain cleanroom access logs aligned to ISO 14644 classifications where used. If electrical compatibility matters, list the EMC testing standards you follow (for example: IEC 60601-1-2 sub-chapters on immunity and emissions) and keep test reports linked to batch records. These specific checkpoints stop slow creep from hiding in paperwork.
Common mistakes that accelerate silent drift
– Assuming visual cleanliness equals control. Oils and particulates can be invisible but cumulative. – Mixing tooling across product families. A dedicated set for sensitive components saves rework. – Skipping retention samples because space is limited — that short-term gain costs traceability later. – Relying on single-point inspections instead of lightweight, frequent checks. Avoid these patterns. Also, don’t overcompensate with complex automation that lacks clear failure modes — a simple trap sensor that flags runoff is better than a black-box routine you can’t debug quickly.
Three metrics to choose and trust
1) Contamination incidence per million parts (CIPM): measure any detected contamination events normalized to output. A falling CIPM after a control change is the clearest sign of progress. 2) Mean time between cleanups (MTBC) tied to tool hours: track how often fixtures or spindles require intervention; a rising MTBC signals process stability. 3) Retention-test compliance rate: percent of lots with complete retention and test records (including the 14-day bioburden incubation result where relevant). These three metrics form a compact scorecard for shopfloor resilience and supplier evaluation.
Where this logic ends and value begins
Fixes are rarely dramatic. They are small barriers placed where drift begins — a check, a filter, a documented handoff. Those moves are what I saw validated across technical booths and panel talks at industry shows, and they map back into better yields on the floor. Put the metrics above into a dashboard, enforce two control gates per part family, and audit tool swaps. The steady result is fewer surprises and fewer silent failures.
Closing note
Measure what drifts, stop what accumulates, and make traceability non-negotiable — and you turn latent failures into solvable items. See how practical upgrades performed live at Medtec. Short thought: small discipline, big difference.